Film-Line Edge Trim
Collect clean BOPP trim by film grade. Specify the scrap rate and collection method before sizing an offline recycling line or discussing an integrated feed arrangement.
Products and solutions
Products and solutions onlyNo matching products or solutions found.
BOPP Production Scrap Recycling
Recover BOPP film edge trim, slitting offcuts and rejected reels from film manufacturing and packaging conversion. Combine cutter compaction, extrusion, degassing and water-ring pelletizing to prepare sorted polypropylene scrap for reuse trials or sale as recycled pellets.
Start with the source and form of the scrap, then choose the feeding and melt-treatment configuration.
Collect clean BOPP trim by film grade. Specify the scrap rate and collection method before sizing an offline recycling line or discussing an integrated feed arrangement.
Recover loose strips and cut-outs from converting operations. Keep unprinted material separate from printed, coated and laminated batches.
Prepare off-spec rolls and reel ends for controlled feeding. Share reel dimensions and core type so unwinding or size reduction can be specified separately.
BOPP means biaxially oriented polypropylene. Identify the complete film structure, not just the outer layer.
| Scrap Stream | Preparation | Configuration Focus |
|---|---|---|
| Clean, unprinted BOPP trim | Separate by grade, colour and production batch; remove foreign material. | Stable compactor feeding and melt filtration matched to the intended PP reuse. |
| Off-spec BOPP reels and reel ends | Remove cores, tape and labels; confirm how the film will be unwound or reduced. | Feeding equipment sized for reel dimensions and the required batch throughput. |
| Printed, coated or metallized BOPP | Keep separate from clear film and provide representative samples. | Assess degassing, filtration, odour, colour and residue limits through trials. |
| BOPP/PE or other laminated film | Identify every polymer layer, adhesive and coating before evaluation. | Confirm process suitability and an outlet for the mixed material; do not assume pure PP output. |
The pelletizing line accepts prepared scrap. Washing, reel preparation and direct connection to a film production line are separate project requirements, not standard functions of every configuration.
The core process stays the same; feeding, operating settings and filtration follow the actual scrap batch.
Identify the film grade and remove cores, labels, tape and foreign objects. Meter prepared loose scrap into the compactor; define roll handling separately.
The cutter compactor reduces film size and raises bulk density to provide a more consistent feed to the extrusion screw.
Melt the prepared film, use vacuum degassing to reduce moisture and volatile residues, and filter solid contaminants within the selected screen capability.
Water-ring die-face cutting forms pellets for cooling, drying and collection. Sample each batch before release for reuse or sale.
Consistent collection and a defined pellet specification make equipment selection more reliable.
Cutter compaction conditions low-bulk-density strips and offcuts before extrusion. Feeding trials establish a practical throughput for your material.
Separate clear, printed and coated batches at collection. This preserves options for pellet colour, formulation and downstream use.
Choose degassing and filtration against moisture, coating load and pellet acceptance criteria. Avoid selecting a line by nominal output alone.
Review the equipment arrangement and agree on pellet acceptance using a sample of your own scrap.
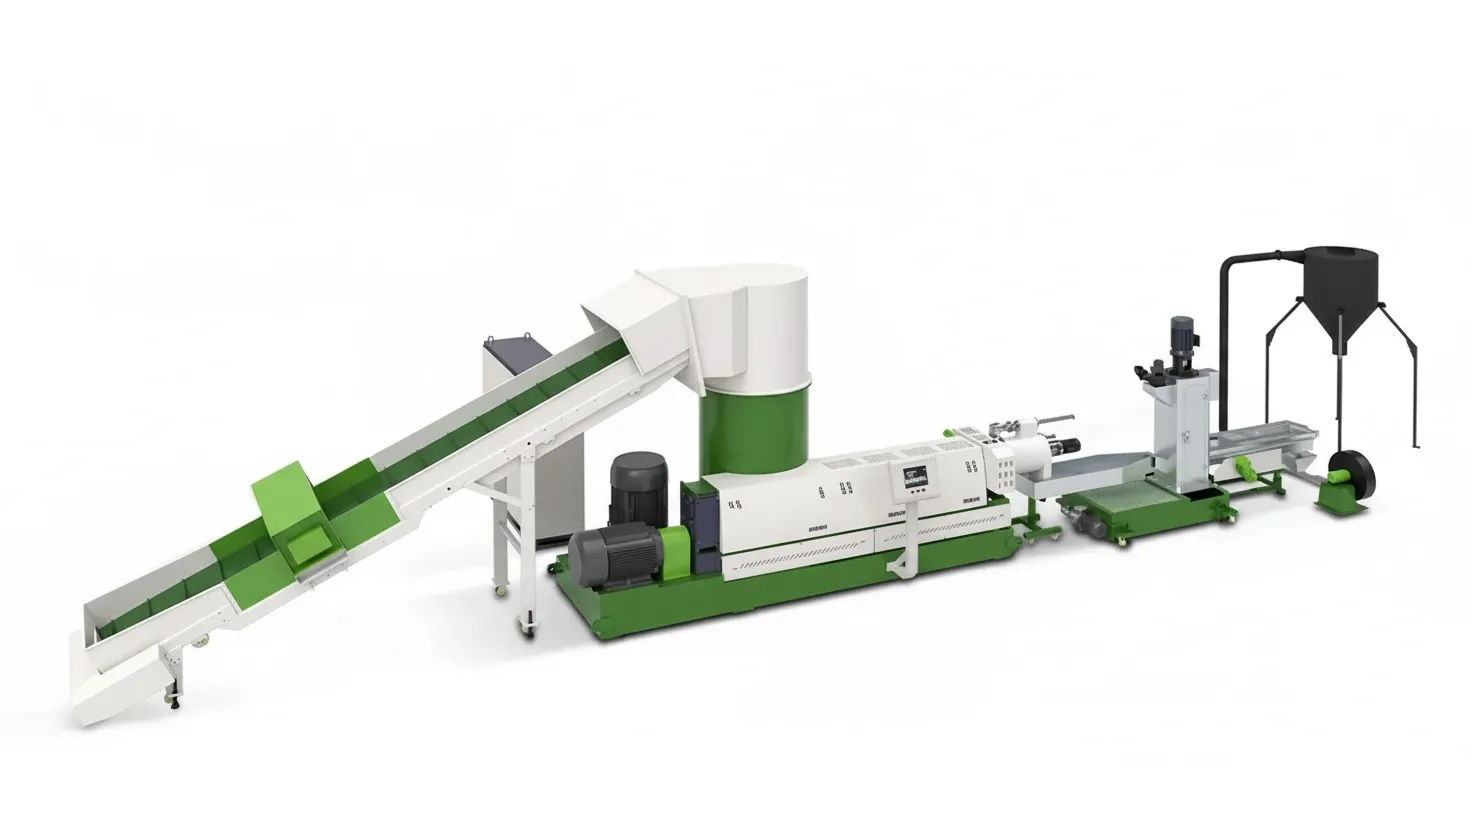
The cutter compactor, extrusion section, filtration and water-ring cutting modules form the core of the BOPP scrap recycling system.
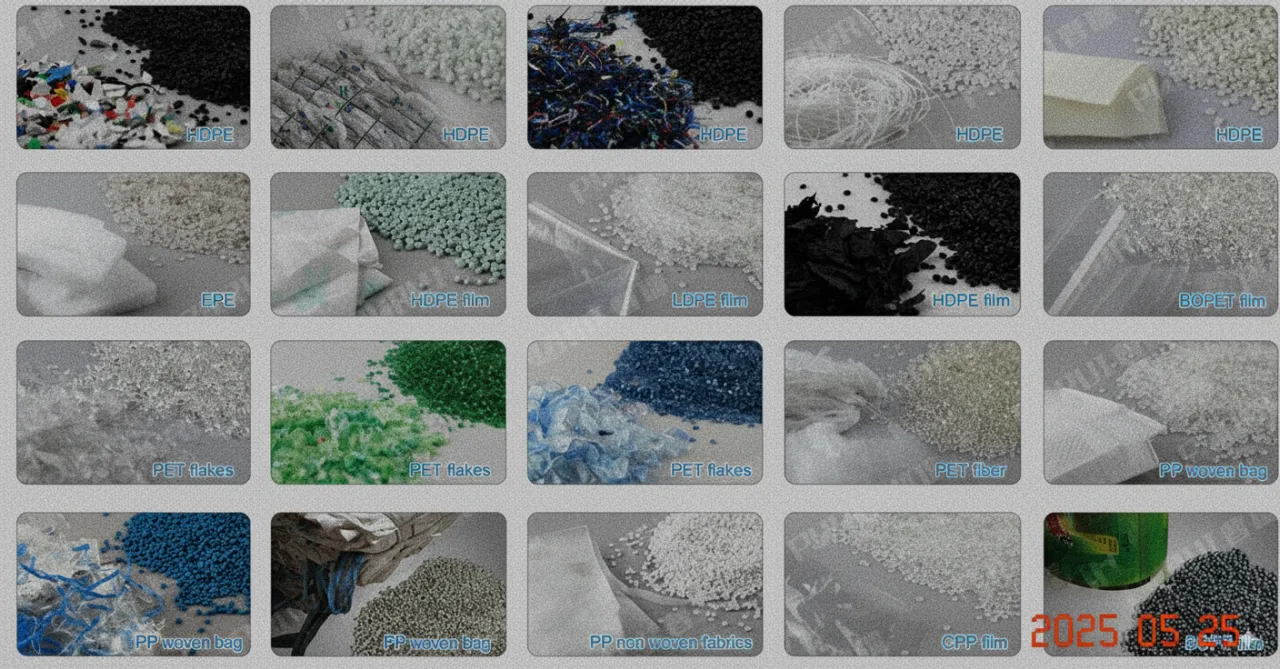
The pellet image is illustrative, not a BOPP trial result. Confirm melt flow, colour, odour, contamination and handling properties with pellets made from your feedstock.
Use a dedicated collection and recycling plan for each production waste stream.
Recycle segregated edge trim and off-spec film. Evaluate recycled PP for a defined formulation and production trial.
Consolidate narrow strips, roll ends and rejected reels by film structure before preparing them for pelletizing.
Assess BOPP-based printing rejects and converting offcuts separately according to ink, coating and laminate composition.
Build traceable batches from known factory sources and agree on the pellet specification with the receiving manufacturer.
Existing model range. Motor power and auxiliary equipment are finalized after material testing.
| Model | Screw Diameter | L/D Ratio | Motor Power | Output Capacity |
|---|---|---|---|---|
| ML95 | 95 mm | 30:1 / 32:1 | Project specific | 300-450 kg/h |
| ML110 | 110 mm | 30:1 / 32:1 | Project specific | 450-650 kg/h |
| ML130 | 130 mm | 30:1 / 32:1 | Project specific | 650-900 kg/h |
| ML160 | 160 mm | 30:1 / 32:1 | Project specific | 900-1,100 kg/h |
Listed capacities are reference ranges. Actual throughput depends on film form, bulk density, grade, moisture, coatings, filtration and the required pellet quality. Reel handling and film-line integration must be specified separately.
A representative sample and production data are more useful than a machine capacity alone.
List PP grades, thickness, print coverage, coatings and any laminate layers. Include moisture, storage conditions and representative scrap photos.
Describe loose trim, collected strips or reels. Share reel dimensions, daily quantity, operating hours and the target recycling rate in kg/h.
Provide available floor space, utilities and collection method. State whether recycling will be offline or needs a separately engineered production-line connection.
Identify the intended buyer or reuse process, melt-flow range, colour and contamination limits, and any planned virgin-resin blending trial.
Use the same representative scrap for process trials and downstream evaluation.
| Check | What to Evaluate | Why It Matters |
|---|---|---|
| Melt flow | Measure recycled PP melt flow under agreed test conditions. | Helps determine suitability for the receiving process and formulation. |
| Gels & solid contamination | Inspect pellet samples and, where relevant, a trial film for gels and specks. | A visually uniform pellet alone does not establish film quality. |
| Colour & odour | Compare clear, printed and coated batches against the agreed specification. | Degassing and filtration do not guarantee decolourization or complete odour removal. |
| Downstream performance | Run the proposed reuse application and blending ratio with the trial pellets. | Confirm the actual product properties before planning routine material return. |
Yes. Sorted BOPP film trim can be compacted, melted, filtered and pelletized for evaluated PP applications. The film grade, additives and contamination determine the pellet properties and suitable reuse options.
Reels need an agreed preparation and feeding method. Provide reel width, diameter, weight and core type so unwinding or size reduction can be specified. Remove cores and foreign material; whole-reel feeding is not assumed in the standard line.
Clean, dry, source-separated production scrap may be suitable for direct pelletizing after preparation. Material contaminated with dirt, labels, moisture or other waste may need cleaning and drying first. Confirm the route using representative samples.
These streams require separate assessment of ink, coating, adhesive and polymer composition. Degassing can reduce volatile residues and filtration can capture some solids, but neither guarantees removal of every coating or separation of laminate polymers. Approve the configuration and pellet outlet through material trials.
Possible reuse depends on the film formulation and quality limits. Test melt flow, gels, colour and downstream film performance, then establish an acceptable blending ratio. Pelletizing alone does not guarantee suitability for BOPP film or a particular packaging specification.
The page describes a pelletizing system for prepared production scrap. A direct connection to a film line, continuous trim collection or automatic synchronization needs separate engineering. Share the production speed, trim rate and available layout before selecting that arrangement.
BOPP is polypropylene, while stretch film is commonly polyethylene. Keep these streams identified and select operating conditions and pellet acceptance criteria for the actual resin. The PE packaging film page covers the separate stretch film, bag offcut and pallet-wrap applications.
Start with scrap quantity per shift, recycling hours, feed form and the required pellet quality. The listed models cover reference capacities of 300–1,100 kg/h; confirm achievable output with your film and chosen filtration before final sizing.
Send your film structure, scrap photos, reel or trim details and hourly target. We can assess preparation, compactor feeding, melt treatment and the trial criteria for your pellet outlet.